Home » Products » Pipe Fittings, Valves & Pumps » Butt Weld Pipe Fittings

Butt Weld Pipe Fittings Manufacturer

Carbon steel elbows, tees and reducers for wholesale piping orders

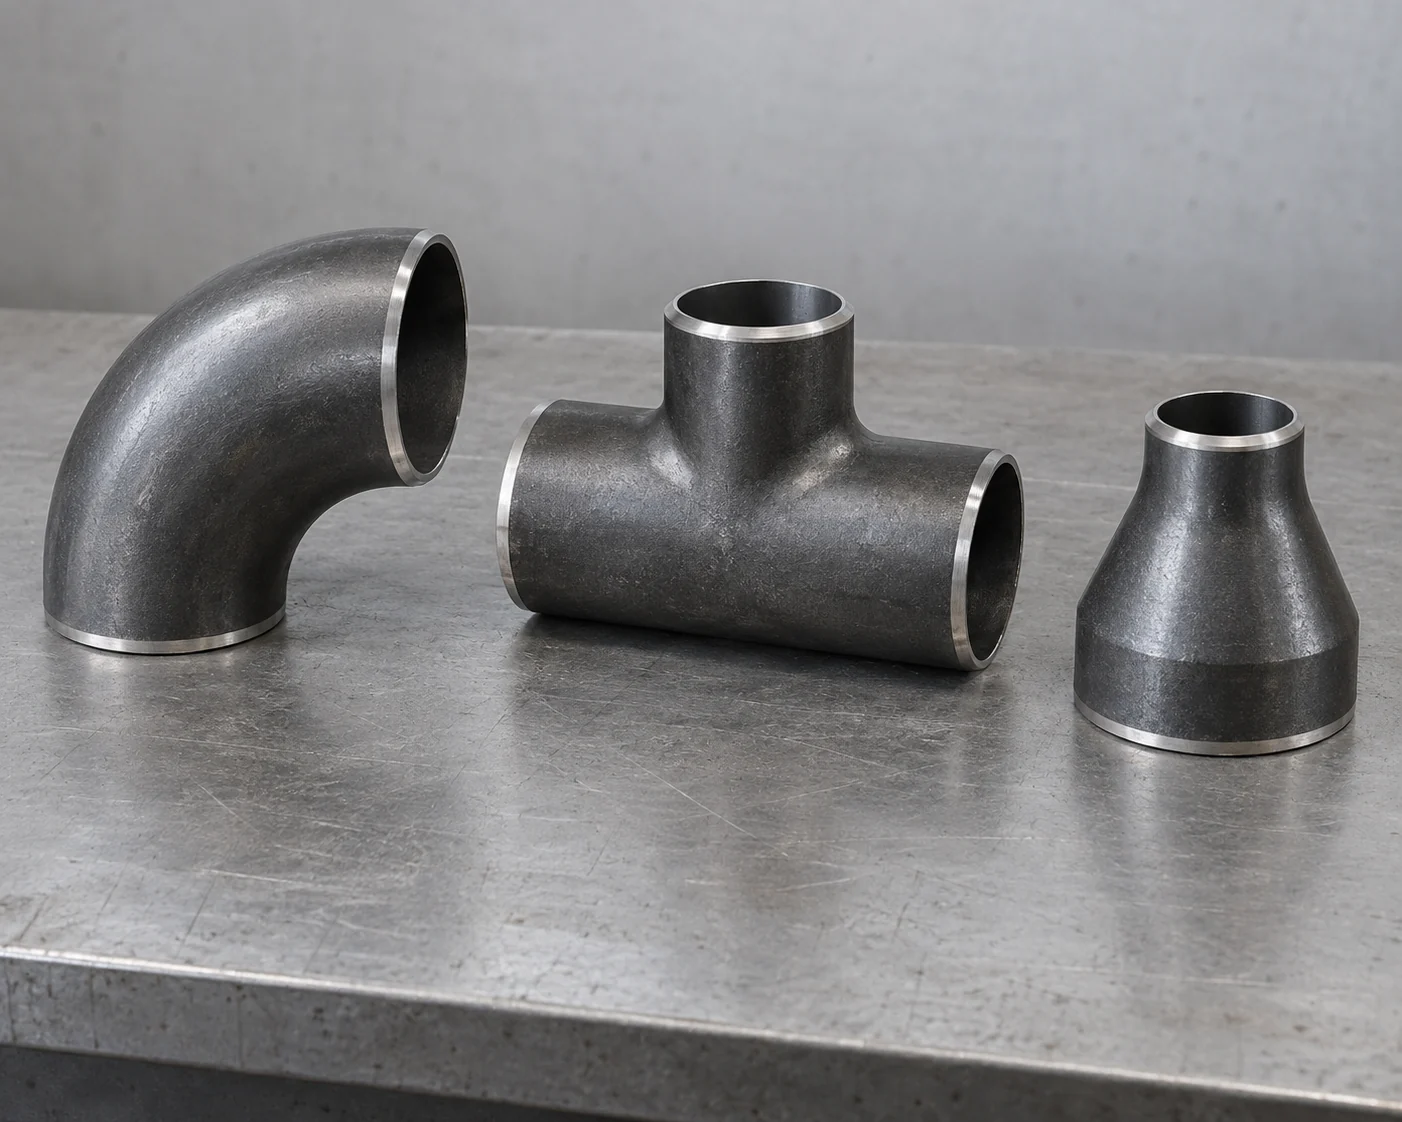
Long-radius elbows, equal and reducing tees, and concentric or eccentric reducers form our carbon steel butt weld fitting range. Beveled ends prepare the fittings for welded pipework, with size and wall schedule matched to the adjoining pipe.

Seamless size range
1/2–24 in.
Core material
ASTM A234 WPB
Dimensions
ASME B16.9
Connections
Beveled weld ends

Elbows, Tees and Reducers

45° and 90° elbows

Long-radius 45° and 90° elbows are supplied to the specified spool layout. Short-radius elbows are quoted as separate patterns for restricted-space connections.

Equal and reducing tees

An equal tee has the same nominal size at all three ends. A reducing tee has a smaller branch: a 6 × 4 in. tee has a 6 in. run and a 4 in. branch. The branch size stays on the order line.

Concentric and eccentric reducers

Both types connect two pipe sizes. A concentric reducer keeps their centerlines aligned; an eccentric reducer offsets the smaller end. The piping drawing establishes the type and orientation.

Material specificationASTM A234 WPB carbon steel
Core seamless rangeNPS 1/2–24 in.; size and wall schedule listed by fitting type
Dimensional standardASME B16.9
Weld-end preparationASME B16.25 or the specified connection drawing
Surface protectionRust-preventive oil or specified protective coating
Quantity basisPieces for each fitting type, size and wall designation

Butt weld fitting sizes and fabrication dimensions

Find the pipe size, weld-end diameter and fitting takeout.

ASME B16.9 layout reference — dimensions in millimeters
NPS (in.)Weld-end OD (mm)Sch 40 end wall (mm)90° LR center-to-end (mm)45° LR center-to-end (mm)Equal tee center-to-end (mm)
260.33.91763564
388.95.491145186
4114.36.0215264105
6168.37.1122995143
8219.18.18305127178
10273.09.27381159216
12323.810.31457190254

No matching size. Clear the search to see the full range.

Scroll sideways to see every column.

The wall column gives the nominal Schedule 40 connection thickness. Center-to-end values locate the fitting ends relative to the pipe centerline intersection. These reference dimensions support layout checks; the purchase schedule identifies the ordered grade, construction and wall.

4 in. fittings occupy different lengths

A 4 in. long-radius 90° elbow has a 152 mm center-to-end dimension. The 45° elbow is 64 mm, and an equal tee is 105 mm. The common 114.3 mm weld-end diameter does not make their fabrication takeouts interchangeable.

Reducer sizes and centerline alignment

ASME B16.9 reducer layout reference
Large × small NPS (in.)Large-end OD (mm)Small-end OD (mm)End-to-end length (mm)
2 × 1-1/260.348.376
3 × 288.960.389
4 × 3114.388.9102
6 × 4168.3114.3140
8 × 6219.1168.3152
10 × 8273.0219.1178
12 × 10323.8273.0203

The listed end-to-end lengths apply to both concentric and eccentric reducers of these sizes. Wall schedules are specified for the connection at each end, independently of the length shown here.

Aligned pipe centerlines

A concentric reducer places both openings on one axis. For a 6 × 4 in. transition, the weld-end ODs are 168.3 and 114.3 mm and the reference length is 140 mm.

Offset pipe centerlines

An eccentric reducer has an offset small end and one straight side. Its orientation affects high and low points in the line, so the flat-side position remains part of the installation drawing.

Two pipe-end schedules

A reducer connects two pipe sizes that may also have different nominal walls. Both size and wall entries belong on the fitting line; the large-end schedule alone does not describe the second weld connection.

Pipe Wall and Weld-End Preparation

Wall designations that differ at larger sizes
NPS (in.)DesignationNominal end wall (mm)Compared designationNominal end wall (mm)
12STD9.53Schedule 4010.31
10XS12.70Schedule 8015.09

These nominal pipe-end wall references show why STD and XS cannot be substituted for Schedule 40 and 80 across the full size range.

Outside diameter and end wall

A matching NPS establishes the outside-diameter series. The pipe and fitting end walls then determine the weld connection detail. A change in wall requires the transition specified on the approved joint drawing.

Bevel and root face

The bevel prepares the edge for welding while the root face retains metal at the bore. ASME B16.25 covers different preparations for different wall conditions; the order carries the required end detail.

Welding and spool assembly

We supply the fitting with its specified ends. Field welds and spool fabrication follow the purchaser’s welding procedure and approved layout, including any required examination of the completed joints.

Match fittings with our seamless carbon steel pipe range

Material certificates and project release records

Material test results

The material certificate records the supplied heat, chemical composition and mechanical test results. Those results are checked against the specified A234 grade and any additional purchase requirements.

Welded fitting examination

A welded fitting order identifies the required weld examination and its acceptance criteria. The examination report belongs to that construction scope; it is separate from the field-weld inspection of the completed piping.

Forming and heat treatment

Forming changes the tube or plate into the elbow, tee or reducer shape. The required heat-treatment condition follows the material specification and manufacturing route; it remains part of the release documentation.

Project submittals

Required manufacturer approval, drawing revisions and special examination are reviewed before production. The agreed document list is included with the fitting order.

Dimensional checks before the fittings are packed

Carbon steel butt weld elbow with a caliper and square on an inspection bench

Weld-end diameter and wall

End measurements check the connection diameter and wall against the fitting schedule. For a reducer, the large and small openings are checked separately.

Center-to-end and end-to-end dimensions

Elbows and tees are checked by their fabrication takeouts; reducers by overall length and opening alignment. The selected radius or branch pattern stays with the inspection item.

Bevels and finished surfaces

Inspection covers the machined weld edges, root faces and visible surface condition. Damage at an edge is addressed before protective packing is applied.

Marking and heat identity

Size, material grade, wall designation and traceability identify the fitting during receiving and fabrication. The packing list keeps that identity with the correct piece count.

Order release documents

Material certificatesDimensional recordsRequired examination reportsPacking list
Wholesale quantities, packing and quotation terms

A separate line for each fitting

A 6 in. 90° LR elbow and a 6 in. 45° LR elbow are separate items, even at the same wall schedule. Tees retain run and branch sizes; reducers retain both end sizes and their concentric or eccentric type. Quantities are counted in pieces.

Protected Bevels and Identified Packages

Packing protects beveled edges during handling and separates fittings by size and pattern. Small items travel in cartons or wooden packing; the shipment list reconciles each package with the ordered fitting lines.

An itemized factory quotation

Our quote states the material, construction, dimensions and piece quantity for each line. Batch quantities, production timing, protective finish, document scope and shipment terms are priced for the requested destination.

Butt weld fittings purchasing questions

Are butt weld fittings rated Class 150 or Class 300?

ASME B16.9 butt weld fittings are not selected by flange pressure class. The material, wall thickness, temperature and piping design code establish the applicable pressure design. Flanged items on the same material list retain their own class designation.

Can you supply short-radius elbows for a restricted layout?

Yes. Short-radius elbows are a separate pattern from the long-radius elbows in the dimension table. The radius, angle and required center-to-end dimension identify the replacement or restricted-space item.

Can a mixed order include pipe and butt weld fittings?

Yes. Pipe lengths and fitting pieces can appear in the same supply order. They remain separate quotation lines, with matching material and weld-end requirements identified for the connected items.

Can you quote a nonstandard angle or fitting drawing?

Yes. A drawing-based inquiry identifies the angle, dimensions, material, end preparation and quantity. We review that fitting separately from the standard B16.9 shapes and state the manufacturing scope on the quotation.

Get a quote for your butt weld fitting list

Send the fitting types, material grade, NPS, wall schedules and piece counts with your delivery destination. Attach a material takeoff or piping drawing for an itemized factory supply quote.

METDAX
Get a quote
Search METDAX

Language

Get a factory quote

Send your specifications or attach a material list.

Butt Weld Pipe Fittings

Your information is used to respond to this inquiry. Privacy policy

ruofan1901@gmail.com